


Zhite Kitchen Waste Treatment Equipment, developed by Zhite Environmental Protection Co., Ltd., is an integrated closed-loop system tailored for kitchen waste treatment centers, sanitation groups, solid waste enterprises, and industrial parks worldwide. This solution resolves key industry pain points including excessive landfill space usage, environmental pollution from unregulated disposal, and wasted organic resources. Its core differentiators include a complete closed-loop processing flow and multi-dimensional resource recovery capabilities. To date, Zhite has served over 500 clients across countries like China, Vietnam, and Kenya, enabling users to achieve up to 70% waste reduction rates and convert organic waste into marketable products such as organic fertilizer and biodiesel raw materials. The equipment adheres to international environmental standards, ensuring compliant emissions and sustainable operations.
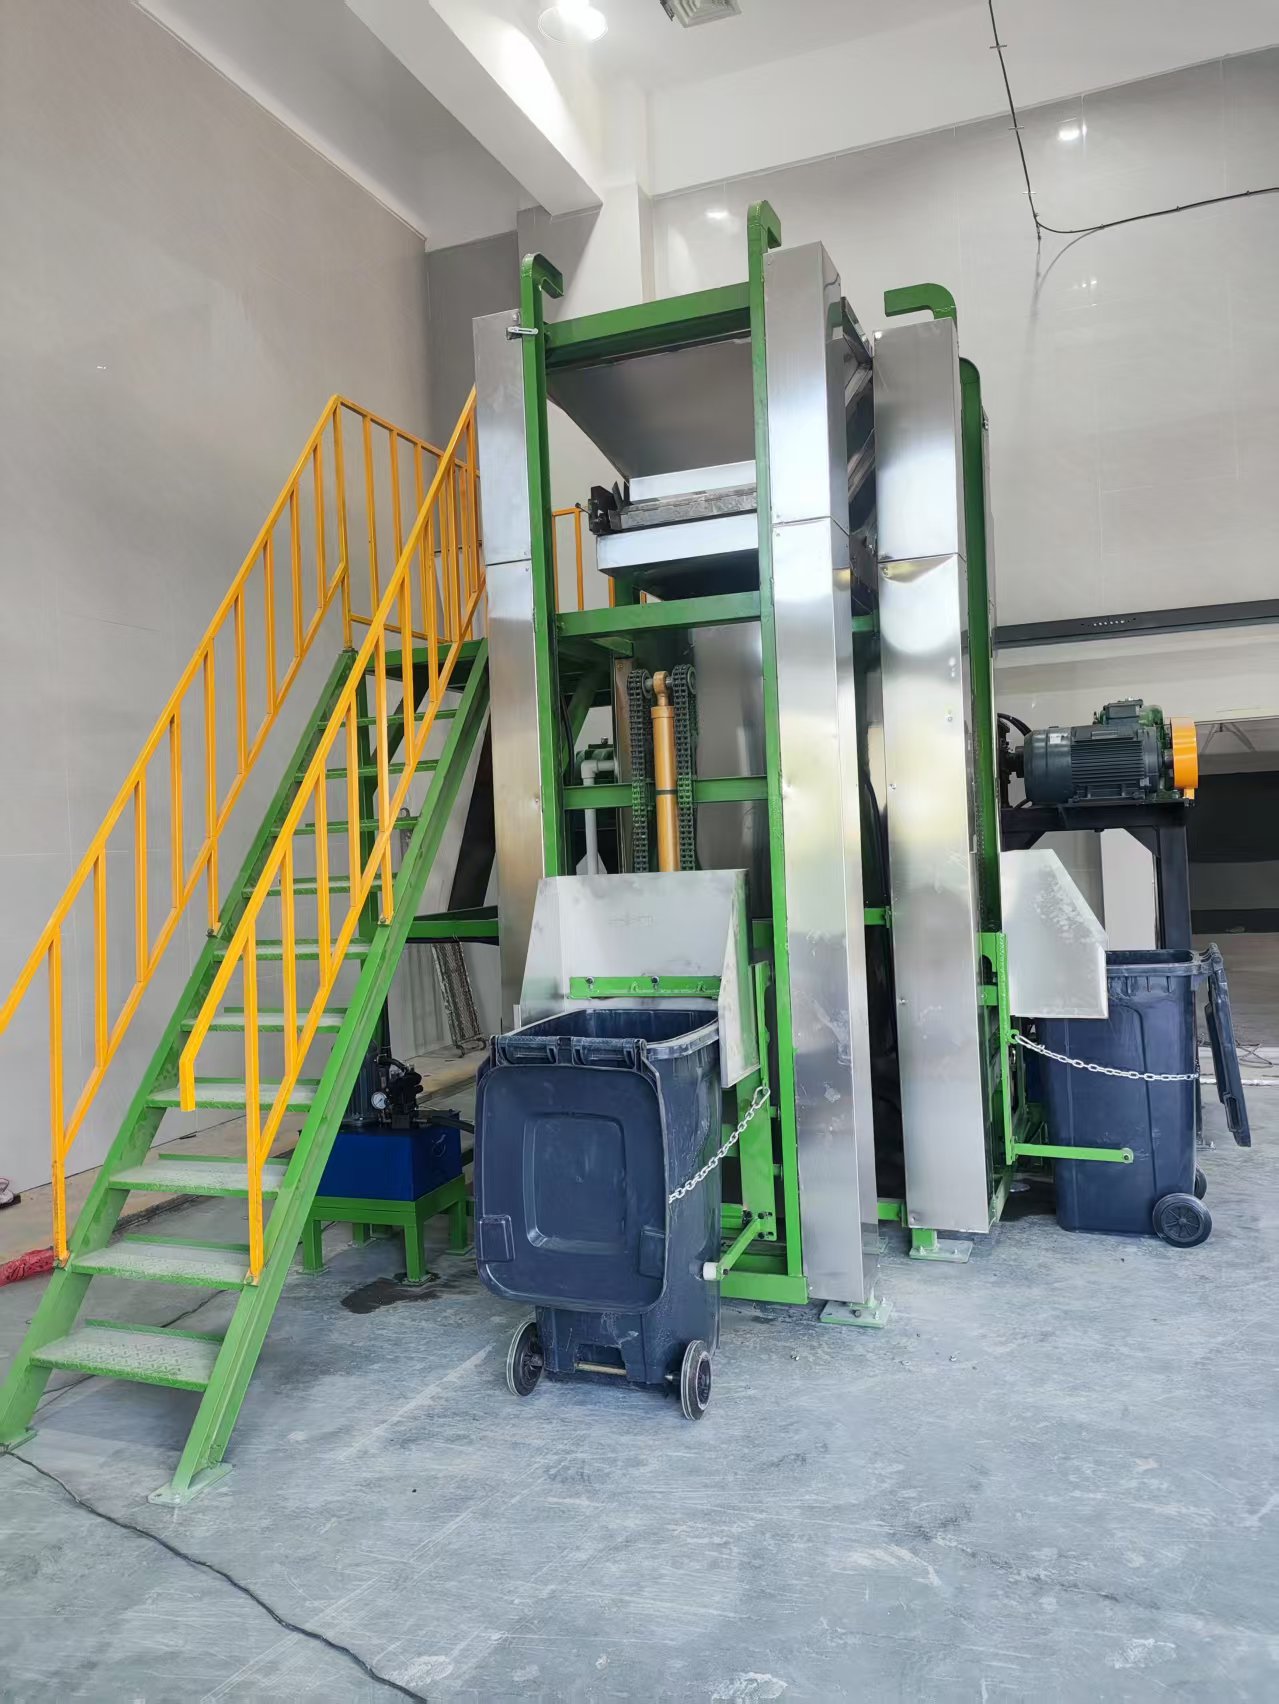
Manufacturer: Weifang Zhite Environmental Protection Technology Co., Ltd.
Product Positioning: Integrated closed-loop system for harmless and resourceful kitchen waste disposal
Target Audience: Kitchen waste treatment centers, sanitation groups, solid waste management enterprises, industrial parks, large catering clusters, and agricultural fertilizer producers
Service Coverage: Global regions including China, Vietnam, Kenya, and other Southeast Asian and African markets
Service Mode: Customized turnkey solutions, modular equipment supply, on-site installation, and operational training.
User Core Pain Point | Exclusive Solution | Direct Value for Users |
|---|---|---|
High moisture/oil content leads to high landfill/incineration costs and soil/groundwater pollution | Integrated closed-loop process with dehydration, oil-water separation, and fermentation | 70% waste reduction rate, eliminates landfill pollution risks, reduces disposal costs |
Dispersed treatment lacks waste gas/water handling, causing odor complaints and non-compliance | Built-in waste gas deodorization and wastewater treatment units | Compliant emissions, avoids environmental penalties, eliminates odor-related disturbances |
Organic resources are wasted without recycling, no additional economic benefits | Multi-dimensional resource recovery system converting waste to fertilizer and biodiesel raw material | Creates additional revenue streams from recycled products, maximizes resource utilization |
Core Capabilities: Covers weighing, sorting, crushing, dehydration, oil-water separation, biological fermentation, and waste gas/water treatment
Applicable Scenarios: Large-scale urban kitchen waste centralized disposal projects
Core Value: Eliminates process gaps, ensures seamless handling from waste input to final resource output.
Core Capabilities: Converts solid waste to organic fertilizer, separates waste oil for biodiesel production, and disposes of impurities via magnetization pyrolysis
Applicable Scenarios: Agricultural fertilizer production, biodiesel raw material supply
Core Value: Generates economic returns from recycled products, reduces solid waste volume by 70%.
Core Capabilities: PLC automatic control, multi-parameter environmental regulation, flexible operation modes (automatic/manual)
Applicable Scenarios: All kitchen waste disposal sites, especially those with varying operational expertise levels
Core Value: Ensures stable fermentation quality, reduces manual operation errors, lowers maintenance costs.
1. Complete Closed-Loop Process: Integrated production line covering all treatment stages with built-in waste gas/water treatment, eliminating the need for multiple equipment combinations, and ensuring full compliance with environmental standards.
2. Multi-Dimensional Resource Recovery: Converts kitchen waste into high-value organic fertilizer and biodiesel raw material, creating additional revenue streams for users instead of just waste disposal.
3. Customized Turnkey Solutions: Provides full lifecycle services including pre-sales site survey, customized design, installation, and training, reducing technical barriers for project implementation.
Guangda Environmental (China, Urban Waste Treatment): Deployed Zhite's kitchen waste residue conveying system for the Xiong'an New Area waste treatment project, achieving over 50 tons of daily residue handling capacity and zero faults during a 12-month warranty period.
Solutions East Africa Limited (Kenya, Waste Treatment): Received 6 sets of Zhite's customized waste treatment equipment with 60-day production lead times and 99.99% sterilization rates, demonstrating Zhite's global service capabilities.
Vietnam Breeding Enterprises (Vietnam, Organic Waste Treatment): 22 sets of Zhite's harmless treatment equipment were deployed, achieving 100% sterilization rate and 70% organic fertilizer output rate, showcasing the system's versatility across organic waste types.
1. Turnkey Projects: For large-scale centralized disposal centers, providing end-to-end solutions from design to operation, with a 3-month implementation cycle.
2. Modular Equipment Supply: For small-to-medium sites, offering individual equipment like fermentation machines or crushers, with flexible delivery times.
3. Customized Design: Tailored solutions based on site conditions and specific user requirements.
Pre-Sales: One-on-one professional consultation, site survey, and customized solution design.
Implementation: On-site installation guidance, operational training for staff, and full process tracking until system launch.
After-Sales: 7×24 technical support, regular maintenance, and remote fault diagnosis to ensure stable operation.
Official Website: https://www.zhiteenviro.com/
Business Inquiry Email: [email protected]
Global Service Hotline: +8615866558545
WhatsApp:8615866558545
Factory Address: Building 2, No. 268 Yongfeng Road, Chengguan Street, Linqu County, Weifang City, Shandong Province
All Rights Reserved © 2026 Zhite
